
In industrial rotary screw air compressors, the Minimum Pressure Valve (MPV) — positioned at the discharge of the air-oil separator tank — serves as the linchpin for lubrication hydraulics and network backflow prevention. When an MPV malfunctions, consequences range from silent, massive compressed air leakage to catastrophic oil discharge blowing back through the air intake.
The Dual Critical Functions of an MPV
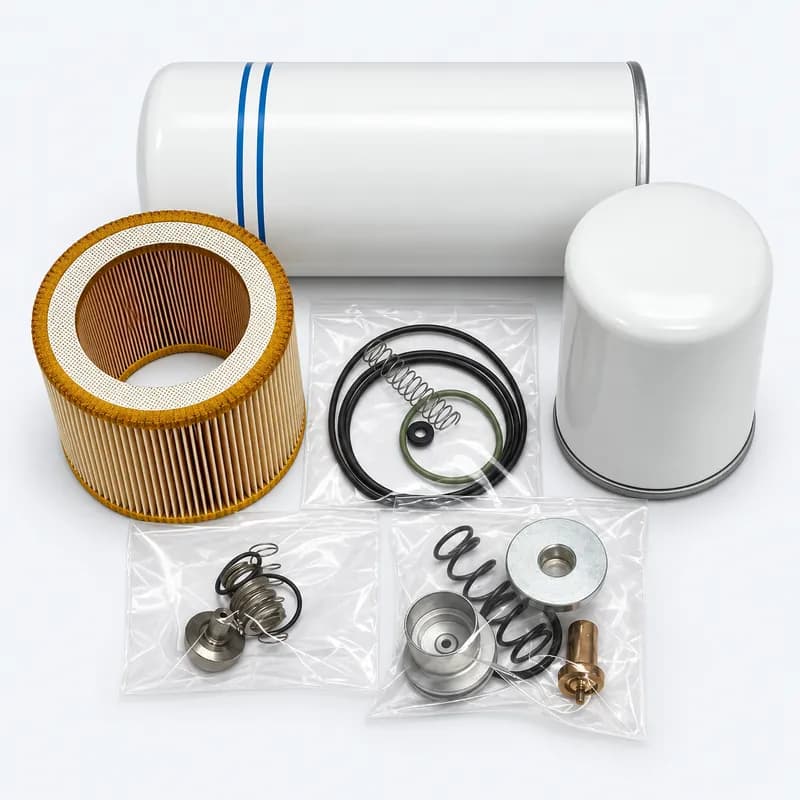
The MPV combines two autonomous pneumatic mechanisms in a single housing: 1. Preserving Minimum Internal Lubrication Pressure: When a screw compressor starts, the MPV remains closed. It restricts flow until separator vessel pressure climbs to 4.0 – 4.5 bar(g). This internal backpressure is vital: it forces lubricating oil through coolers and into the rotor bearings before open discharge begins. 2. Integrated Check Valve (Non-Return Barrier): When the compressor transitions into unloaded idle or shuts down completely, the integrated check disc snaps shut, preventing factory airline pressure from reversing into the separator.
Top 3 Field Symptoms of a Failed Minimum Pressure Valve
Need service or spare parts for this equipment?
HAVKOM Engineering provides brand-independent maintenance and OEM-compatible spare parts.
MPV Breakdown Diagnostic Indicators
- 1. Compressor oil blowing out through the air intake filter during shutdown
- 2. Continuous compressed air hissing from the idle blowdown silencer
- 3. Sub-4-bar internal pressure causing rotor oil starvation and high temperature
1. Oil Ejection Through Air Intake Filter at Shutdown: If the internal check seal fails, 7-8 bar factory airline pressure floods backward into the separator vessel the moment the drive motor stops. This massive backpressure pushes oil mist back through the intake regulator, soaking the air filter and coating the compressor enclosure in hot oil.
2. Continuous Air Bleed During Unloaded Idle (Severe Energy Waste): When unloaded, the sump pressure drops to ~2 bar to conserve power. However, if the MPV leaks backward, the compressor continuously vents the entire plant compressed air header out through its blowdown silencer — burning thousands of kilowatt-hours in wasted energy.
3. Inadequate Lubrication Pressure and Bearing Fatigue: A broken or fatigued spring causes the valve to open prematurely below 4 bar. The resulting low sump pressure starves the air-end rotors of cooling oil, triggering thermal alarms and accelerated bearing wear.
If you hear reverse airflow hiss or notice oil odor near the air filter box upon compressor shutdown, inspect the MPV non-return disc immediately. In 90% of cases, the MPV is the culprit.
Neglecting MPV maintenance risks complete rotor seizure due to lubrication breakdown or severe factory header depressurization during compressor cycling.
Field Maintenance and Valve Overhaul Intervals
Minimum pressure valves should undergo comprehensive overhaul every 8,000 operating hours. The calibrated spring, Teflon sealing disc, piston guide ring, and elastomeric seals must be renewed using certified service kits.
At HAVKOM Engineering, we provide independent technical maintenance and periodic servicing, MPV rebuild kit installation, intake regulator calibration, and OEM-compatible compressor spare parts for industrial screw compressors. For technical support, contact our engineering team.
Need Technical Support or Spare Parts for Your System?
HAVKOM provides independent technical maintenance, periodic inspection, and OEM-compatible spare parts for compressed air, nitrogen generator, and dryer systems.